Join Our Lunch & Learn: How Agentic AI Will Transform Industrial Operations | Register Now →

September 24, 2026
6 Mins
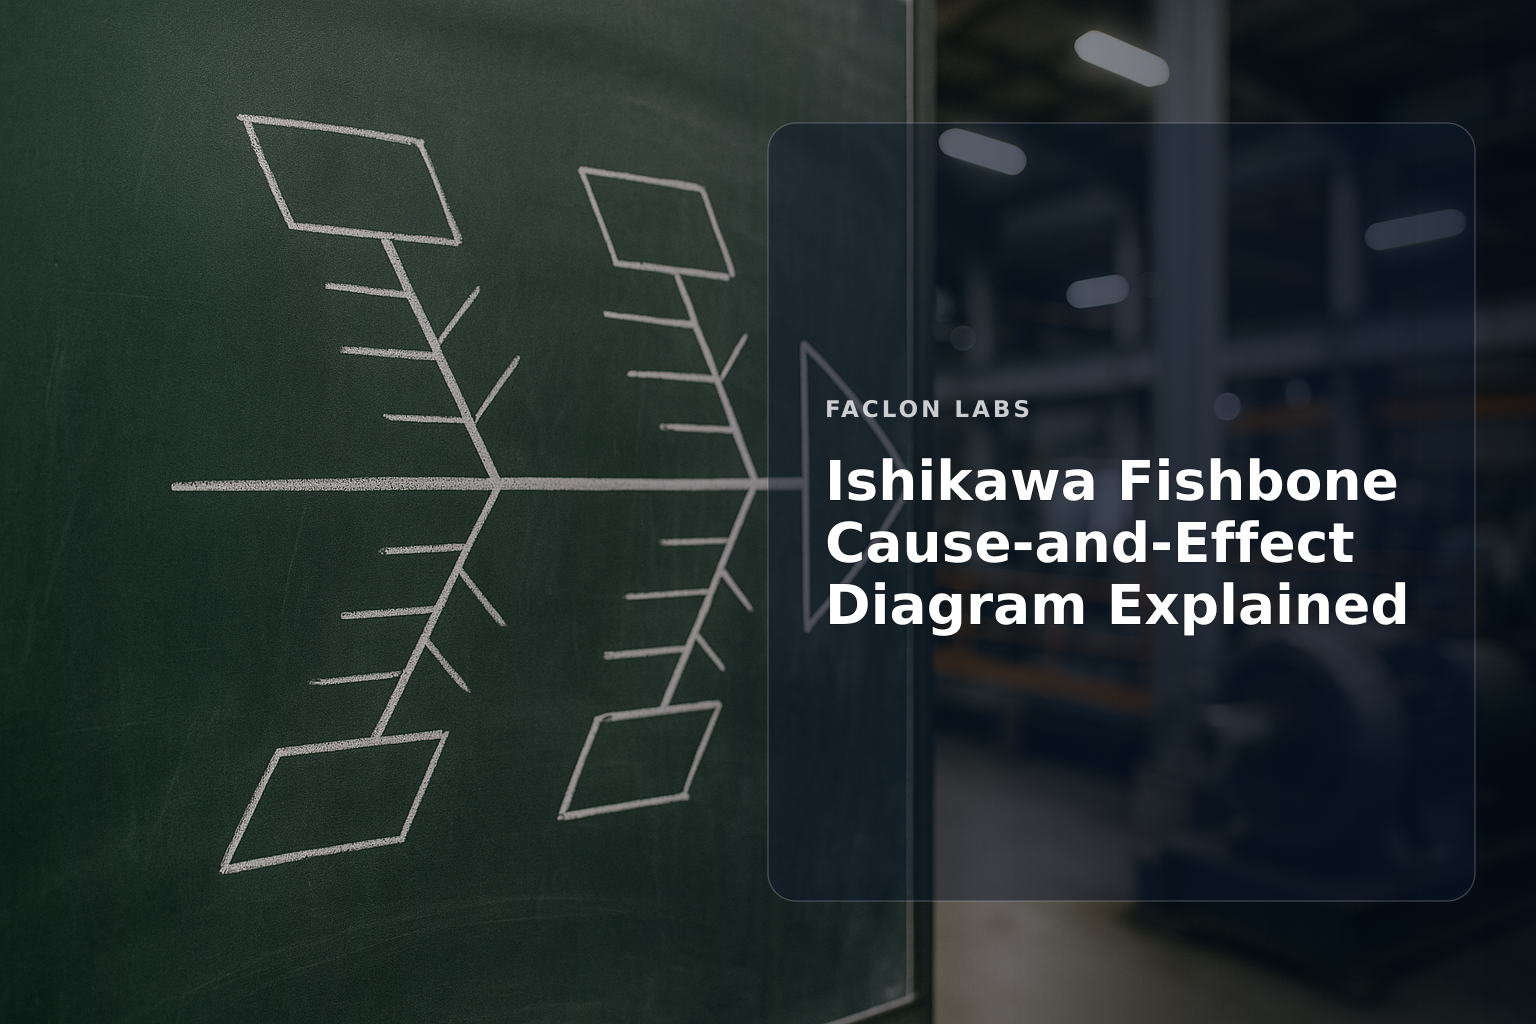
The Ishikawa fishbone cause-and-effect diagram is widely used in industrial environments to clarify the underlying reasons behind operational problems. By organizing causes visually, it promotes collaborative root cause analysis and ensures no critical factor is overlooked. Its structured approach is especially valuable for plant operations leaders aiming to reduce downtime, improve quality, and optimize processes.
Understanding how to construct and apply this diagram with practical steps can empower teams to move from symptom identification to actionable insights. Integrating this method with industrial AI and IIoT data further enhances problem-solving effectiveness in modern manufacturing settings.
The Ishikawa diagram, also called the fishbone or cause-and-effect diagram, was created by Japanese quality control expert Kaoru Ishikawa in the 1960s. It was designed to support quality improvement by visually mapping causes leading to a specific problem or effect.
The diagram resembles a fish skeleton, with a central "spine" and branching "bones" representing cause categories. The "effect" or problem sits at the fish’s head, while causes branch off like ribs, illustrating their relationship to the effect.
Its primary function is to guide teams through a structured brainstorming process, ensuring all possible causes are considered and organized logically. This prevents jumping to conclusions and helps uncover root causes rather than symptoms.
In industrial settings, the diagram fosters cross-functional collaboration, improves clarity around complex problems, and supports comprehensive analysis. It helps teams prioritize interventions that deliver measurable operational improvements [Ishikawa's Fishbone / Cause and Effect Diagram Summary and Forum].
The diagram starts with a precise problem statement placed at the head of the fish. Defining this effect clearly is critical to focus analysis efforts.
The central spine runs horizontally, with major cause categories branching off as "bones." These categories group related causes, making the diagram organized and easy to navigate.
A standard approach uses the 6Ms to categorize causes:
Each major category can be further broken down into sub-causes. These finer details are connected as smaller branches, showing cause-and-effect relationships clearly.
Write a concise, measurable problem statement that everyone agrees on. Example: "Excessive unscheduled downtime on Production Line A."
Draw a horizontal arrow pointing to the problem statement (the fish’s head). Then add diagonal lines off the spine for each major cause category.
Use the 6Ms or other relevant categories for your industry. Engage a cross-functional team to ensure diverse perspectives.
Brainstorm all possible causes within each category. Encourage specific, fact-based entries rather than assumptions.
For each cause, ask "Why?" up to five times to uncover deeper root causes. Add these as sub-branches.
Review the completed diagram to identify the most likely root causes. Prioritize based on impact and feasibility for corrective action.
| Step | Action | Key Focus | Tools / Metrics |
|---|---|---|---|
| 1 | Define Problem | Clear, measurable effect | Problem statement, operational data |
| 2 | Draw Diagram | Visual structure | Diagram template or software |
| 3 | Brainstorm Categories | Major cause groups | 6Ms or customized categories |
| 4 | Identify Causes | Specific potential causes | Team workshops, process maps |
| 5 | Apply 5 Whys | Root cause depth | Root cause analysis techniques |
| 6 | Prioritize Causes | Impact and actionability | Pareto analysis, expert judgment |
The plant experiences frequent unexpected stops, affecting output and costs.
| Category | Example Causes |
|---|---|
| Manpower | Insufficient training, shift fatigue |
| Methods | Inadequate preventive maintenance schedule |
| Machines | Bearing failure, sensor malfunction |
| Materials | Substandard parts, delayed supplies |
| Measurement | Faulty downtime logging, inaccurate sensors |
| Mother Nature / Environment | High humidity affecting equipment |
For Machines: Bearing failure → poor lubrication → missed lubrication schedule For Methods: Inadequate PM schedule → lack of documented procedures → no accountability
The analysis highlights maintenance scheduling and training gaps as root causes, guiding targeted interventions to reduce downtime [Root Cause Analysis Course – Failure Investigation & RCA Training].
Sensor data from machines and environmental monitors provide real-time inputs for the Machines and Mother Nature categories. This data helps validate or refute hypothesized causes.
AI models can analyze patterns in the data to predict failures before they happen, allowing preventive actions aligned with root cause findings.
Faclon Labs’ industrial AI platform aggregates IIoT data, enabling dynamic fishbone analysis with up-to-date metrics and visualizations, streamlining root cause investigations.
Combining fishbone diagrams with AI-driven insights transforms troubleshooting into continuous improvement, minimizing downtime and improving operational efficiency [Fishbone Diagram: Ishikawa & Cause-Effect | Vaia].
Engage operators, maintenance, quality, and engineering to capture all relevant causes.
Maintain a blameless culture to encourage open, honest analysis.
Use tools like the 5 Whys to dig deeper beyond obvious issues.
Best for complex problems with multiple potential causes. Not ideal for very simple or well-understood issues.
Visualizing Production Issues with a Pareto Graph Understanding Energy Consumption in Industrial Plants Essential Tools for Data Analytics in Smart Manufacturing
If you want to improve your plant operations by identifying and addressing root causes effectively, start using the Ishikawa fishbone cause-and-effect diagram combined with industrial AI insights. Faclon Labs can help you integrate these tools into your workflow for measurable operational improvements.
The primary purpose of an Ishikawa Fishbone Diagram is to visually organize and explore all potential causes of a specific problem or 'effect.' It facilitates structured brainstorming, helping teams move beyond symptoms to identify the underlying root causes, thereby enabling more effective problem-solving and process improvement.
The 6Ms are common categories used as the major 'bones' in a Fishbone Diagram, particularly in manufacturing and industrial settings. They stand for Manpower (people), Methods (processes), Machines (equipment), Materials (raw materials, components), Measurement (inspection, data collection), and Mother Nature (environment, external factors). These categories provide a comprehensive framework for cause identification.
An Ishikawa Diagram aids root cause analysis by providing a structured visual framework to systematically categorize and explore all possible contributing factors to a problem. By breaking down potential causes into distinct categories and then drilling down with techniques like the '5 Whys,' it helps teams uncover the fundamental issues rather than just addressing superficial symptoms, leading to more sustainable solutions.
Yes, while often used reactively to solve existing problems, an Ishikawa Diagram can also be used proactively. By analyzing potential failure modes or desired outcomes, teams can brainstorm what might cause deviations or what factors are necessary for success. This helps in designing more robust processes, implementing preventative measures, and identifying key performance indicators to monitor.
